


What is Two Shot Molding?
Definition of Two Shot Injection Molding
Two-shot molding, also known as 2K injection molding or two-color injection molding, is a manufacturing process that involves injecting two different types of plastic materials into a single mold in two distinct stages. This technique allows for the creation of a single part that can exhibit varied properties, colors, or textures. The process is executed using a specialized 2K injection molding machine designed to accommodate multiple shots of different materials, enabling the production of complex designs with enhanced functionality.
Two-shot molding, also known as 2K injection molding or two-color injection molding, is a manufacturing process that involves injecting two different types of plastic materials into a single mold in two distinct stages. This technique allows for the creation of a single part that can exhibit varied properties, colors, or textures. The process is executed using a specialized 2K injection molding machine designed to accommodate multiple shots of different materials, enabling the production of complex designs with enhanced functionality.
How Two Shot Molding Works
-
First Shot Injection: The initial material, typically a rigid plastic like polypropylene (PP) or acrylonitrile butadiene styrene (ABS), is injected into the mold. The mold is shaped to hold the material until the second injection occurs.
-
Material Curing: After the first material has been injected and cooled, the mold rotates to align with the system for the second shot.
-
Second Shot Injection: A second material, often a softer plastic such as thermoplastic elastomer (TPE) or rubber, is injected over the first layer, bonding the two materials together to form the final part. This dual-material approach enhances the tactile qualities or grip of the product.
-
Cooling and Ejection: Once both materials have been injected and bonded, the part is cooled and subsequently ejected from the mold.
Advantages of Two Shot Molding
- Reduced Part Count: By combining two materials in one step, the need for secondary assembly processes is eliminated.
- Enhanced Product Strength: The dual-material structure can improve the part’s durability, providing rigidity where necessary and flexibility where desired.
- Improved Aesthetics: This process enables the creation of multi-colored or multi-textured parts, enhancing visual appeal.
- Cost-Effective for High Volumes: While initial setup costs may be high, the efficiency of the process makes it cost-effective for large production runs.
What is Overmolding?
Definition of Overmolding
Overmolding is a manufacturing technique where one material is molded over another to create a part that leverages the benefits of both materials. Typically, a rigid plastic serves as the base, while a softer, more flexible plastic is molded over it to enhance functionality or aesthetics.
Overmolding is a manufacturing technique where one material is molded over another to create a part that leverages the benefits of both materials. Typically, a rigid plastic serves as the base, while a softer, more flexible plastic is molded over it to enhance functionality or aesthetics.
How Overmolding Works
-
Base Material Injection: The first material, usually a hard plastic like ABS, is injected into the mold to form the core of the part, providing structural integrity.
-
Mold Rotation or Transfer: After the base material cools, the mold is either rotated or the part is transferred to a secondary mold for the second injection.
-
Second Material Injection: A different material, such as TPE, silicone, or rubber, is injected over the base to add features like a soft touch, improved ergonomics, or additional protection.
-
Cooling and Ejection: The part is cooled and ejected from the mold, ready for use.
Advantages of Overmolding
- Improved Ergonomics: Overmolding facilitates the creation of parts with soft-touch surfaces, enhancing comfort and usability.
- Enhanced Durability: The outer layer can provide additional protection, such as abrasion or water resistance, depending on the material used.
- Cost-Effective for Small Runs: This method is ideal for low- to medium-volume production due to its simpler setup compared to two-shot molding.
- Design Flexibility: Overmolding allows for the creation of multi-material parts, balancing rigidity and flexibility where needed.
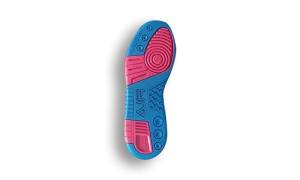
Two Shot Molding vs Overmolding: Key Differences
Material Considerations
- Two Shot Molding: Utilizes two distinct materials injected in separate stages, selected for their specific bonding properties and molded with high precision.
- Overmolding: Involves injecting a second material over an existing molded part, typically a rigid core with a flexible outer layer.
Process Complexity and Cost
- Two Shot Molding: Requires specialized 2K injection molding machines, making it more complex and costly. However, it becomes cost-effective for high-volume production.
- Overmolding: Simpler and often requires less specialized equipment, reducing setup costs, making it ideal for smaller production runs.
Design Flexibility
- Two Shot Molding: Offers greater control over material interaction, allowing for complex geometries and precise bonding.
- Overmolding: Provides flexibility for adding soft-touch elements but may be limited by material compatibility.
Bonding Strength
- Two Shot Molding: Achieves strong, durable chemical bonds between materials during the injection process.
- Overmolding: Bond strength depends on material compatibility and surface texture, sometimes requiring additional processing for secure bonds.
| Aspect | Two Shot Molding | Overmolding |
|---|---|---|
| Process Complexity | More complex, requires specialized equipment | Simpler, requires less specialized equipment |
| Production Volume | Best for high-volume runs | Suitable for low to medium-volume runs |
| Material Flexibility | Can combine multiple materials with precise control | Typically involves a rigid base with a soft outer layer |
| Bonding Strength | Strong, chemical bond between materials | Dependent on material compatibility and surface texture |
| Design Flexibility | High design freedom, allows for complex geometries | Limited design flexibility compared to two-shot molding |
| Cost Efficiency | High initial cost, but cost-effective for large volumes | More cost-effective for smaller production runs |
| Applications | Automotive, medical devices, electronics, aerospace | Consumer goods, packaging, hand tools, automotive |
| Benefits | High precision, durability, aesthetic design freedom | Cost-effective, ergonomic designs, protective layers |
| Challenges | High tooling costs, complexity in setup | Bonding issues, material comp |
Applications of Two Shot Molding and Overmolding
Industries That Use Two Shot Molding
- Automotive: For parts like handles, knobs, and bezels where aesthetics and functionality are crucial.
- Medical Devices: In creating tools that require both rigid and soft-touch components, such as surgical instruments.
- Electronics: Used in consumer electronics for components like smartphone cases and remote control buttons.
Industries That Use Overmolding
- Consumer Goods: Commonly found in items like toothbrushes and cooking utensils, emphasizing comfort and grip.
- Packaging: Often used in childproof packaging, where a rigid base is covered with a soft layer for safety.
- Automotive: For producing handles, seals, and certain interior parts that prioritize ergonomics.
Real-World Examples
- Two Shot Molding: A phone case featuring a rigid plastic structure with a soft, grippy rubber layer.
- Overmolding: A power tool with a hard plastic body complemented by a rubberized, overmolded grip.
Summary:
Both two-shot molding and overmolding are effective processes for creating multi-material parts, but they differ in complexity, cost, and application. Two-shot molding is more complex and ideal for high-volume production, offering precise control over material bonding and design flexibility. It’s commonly used in industries like automotive and medical devices. Overmolding, on the other hand, is simpler and cost-effective for smaller runs, focusing on adding ergonomic features or protective layers to a rigid core. Choosing between the two depends on production volume, material compatibility, and the desired functionality of the part.
